
1. Stabilize part geometry
Use consistent walls, gradual transitions, suitable ribs and adequate draft. Thick intersections invite sink while uneven shrinkage creates warpage; both are easier to reduce in the CAD model.
2. Match gate and flow strategy
Gate type and location influence pressure, weld lines, orientation and appearance. Use flow analysis and material data to confirm fill pattern and avoid treating gate design as a late tooling detail.
3. Design balanced cooling and venting
Cooling circuits should follow heat concentration and cavities must vent trapped gas. Uneven temperature drives distortion; insufficient venting causes burns, shorts and unstable filling.
4. Validate with structured trials
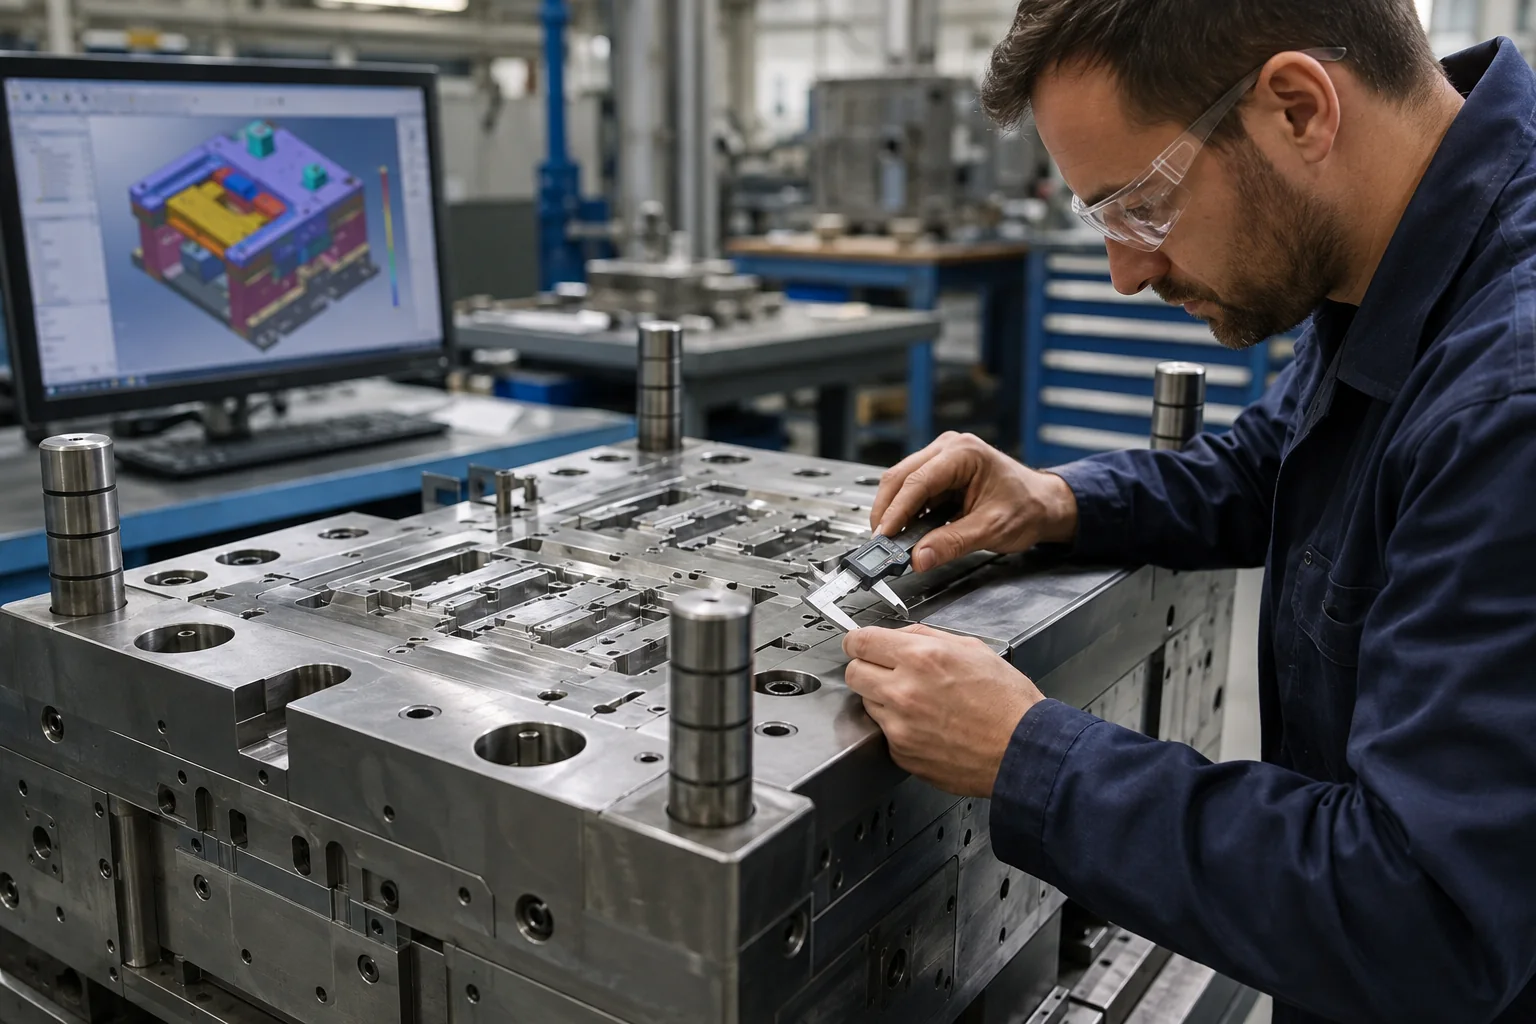
Define trial material, machine, drying, temperatures, pressure, speed and cooling. Record each change separately, measure parts after conditioning and distinguish product, mold and process causes.
Prevention begins before machining
A robust mold is created when the part, tool and process are reviewed as one system. Closing high-risk decisions before steel release reduces correction loops and makes the production window easier to maintain.